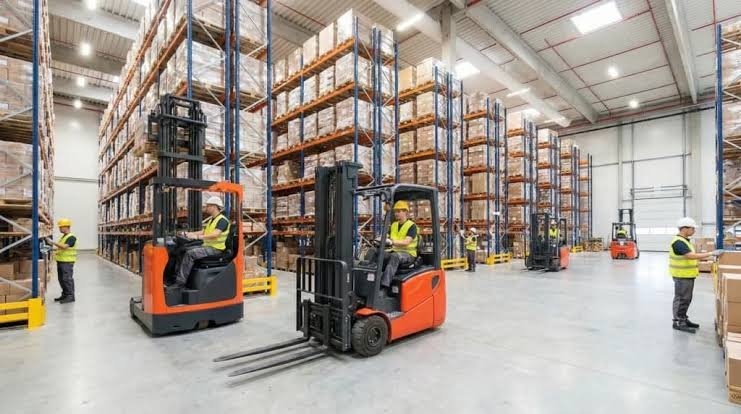
Running a smooth supply chain operation comes down to how well your facility is organized. Whether you manage a small order fulfillment shop or a massive regional distribution center, every square foot of floor space represents overhead cost. When space is wasted or inventory handling slows down, profit margins start to drop. Finding reliable tools to keep goods moving quickly while keeping your workforce safe is one of the single most important tasks for any operations manager.
Setting up a functional industrial space does not always mean buying brand new items straight from the factory floor. Many smart business owners prefer sourcing pre-owned inventory setup items to stretch their capital budgets further. Choosing high quality used warehouse equipment offers an immediate path to increasing storage capacity, improving product accessibility, and streamlining daily picking routines without taking on massive upfront expenses.
Understanding the Value of Pre-Owned Industrial Assets
Upgrading a facility often carries a heavy price tag, especially when expanding dynamic storage systems or adding extra workstations. Brand-new industrial hardware carries hefty manufacturer markups and lead times that can stall projects for weeks or months. Taking advantage of secondary market items allows facilities to expand rapidly while preserving cash flow for inventory and payroll.
Beyond the obvious financial savings, pre-owned industrial assets are ready for immediate deployment. Heavy-duty steel components like structural racks, heavy workbenches, and rolling stairs are built to endure decades of constant use. Buying certified secondary items means you get industrial-grade durability at a fraction of the cost, giving your team immediate access to the structural support they need to handle peak seasonal volume.
Key Operational Categories for Facility Optimization
To build a balanced inventory system, managers must look at how products enter, move through, and exit the building. Every stage of the material handling process requires dedicated tools to minimize manual labor and prevent physical bottlenecks.
Structural Pallet Racking and Storage Shelving
Vertical expansion is the most effective way to multiply usable square footage. Heavy-duty pallet rack systems come in several designs to match specific inventory turn strategies:
- Teardrop Racking: The industry standard for easy assembly, adjustability, and compatibility across various frame styles.
- High-Density Systems: Push-back and drive-in racks maximize volume for high-density inventory setups by reducing aisle counts.
- Cantilever Racks: Ideal for storing bulky, long, or irregular items such as lumber, piping, and metal tubing.
- Industrial Shelving: Perfect for hand-loaded cartons, small parts, and active order-picking zones.
Safe Loading Dock Equipment
The loading dock acts as the front door of your supply chain operations. Keeping this high-traffic area safe and functional prevents costly delays during shipping and receiving hours.
Utilizing durable aluminum dock plates bridges the gap between your concrete staging floor and delivery trailers. These heavy-capacity plates provide a seamless transition for pallet jacks, hand trucks, and foot traffic, keeping your dock workers safe and loading routines on schedule.
Ergonomic Packing Work Tables and Stations
Order fulfillment accuracy begins at the packaging desk. Industrial packing tables combine broad work surfaces with integrated storage shelves to keep boxes, tape, labels, and scanning equipment within arm’s reach. Providing ergonomic work spaces keeps employees comfortable, reduces repetitive stress strain, and speeds up the final packaging process before outbound shipping.
Mobile Maintenance and Picking Ladders
Accessing elevated shelf levels quickly requires heavy-duty mobile ladders. Industrial rolling ladders featuring wide steel steps, safety handrails, and pressure-lock stoppers allow operators to pick loose stock safely from high storage tiers. Smooth-glide wheels allow staff to push equipment across the warehouse floor with minimal physical effort.
How Sourcing Used Warehouse Equipment Accelerates Growth
Every business reaches a point where current storage limits threaten to slow down order processing times. Investing in used warehouse equipment allows growing enterprises to scale operations step by step without overextending cash reserves.
When you source pre-owned material handling assets, you can acquire complete rack configurations, dock tools, and packing setups for less money. This flexibility gives operations managers the freedom to test new floor plan layouts, set up seasonal picking areas, or equip expanded facility wings on short notice.
Best Practices for Evaluating Material Handling Needs
Before placing orders for additional hardware, take time to perform a full audit of your facility floor plan and product inventory patterns. Ask yourself a few basic operational questions:
- What are the weight and dimension profile requirements of your heaviest pallets?
- Are you storing uniform pallet sizes, or do you handle long, irregular materials?
- How many active forklift aisles do you need to maintain continuous traffic flow?
- Do your packing teams have sufficient desk surface area to process peak daily orders?
Matching your hardware choices directly to your physical spatial limits ensures every piece of gear serves a distinct purpose.
Extending Facility Capabilities Through Reliable Sourcing
Upgrading your layout does not require complicated overhauls or excessive capital expenditure. By acquiring secondhand heavy-duty components, business leaders can modernize their facility layout, enhance daily safety standards, and keep goods flowing efficiently out the door.
Integrating trusted used warehouse equipment into your supply chain strategy delivers long-term durability, quick setup times, and massive budget savings. Investing in the right balance of pallet racks, dock transition tools, ergonomic workstations, and mobile ladders builds a dependable workplace ready to handle tomorrow’s growth challenges.